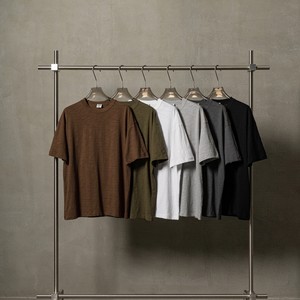
 100% Combed Cotton
Custom Clothing Manufacturers Bulk Men's T-shirts 100% Cotton Knitted
180-240 GSM
Bio-Washed
MOQ 50 Pcs
 Talk to production646-681-4212
Explore our high-demand custom apparel catalog engineered with certified organic cotton, performance synthetic knits, and precision flatlock seam construction.
100% Combed Cotton
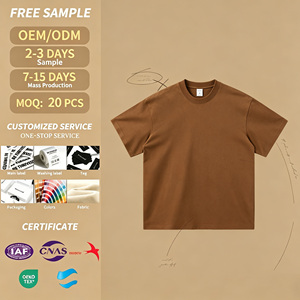 Cut & Sew Fleece
 3D Puff Embroidery
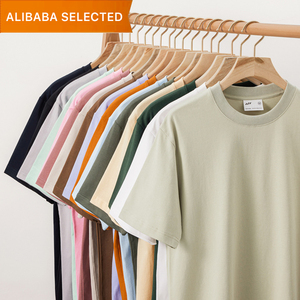 Heavyweight 250GSM
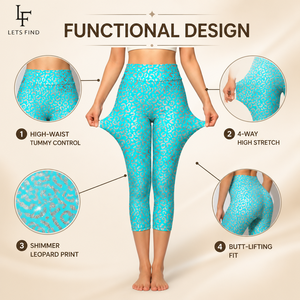 4-Way Stretch Nylon
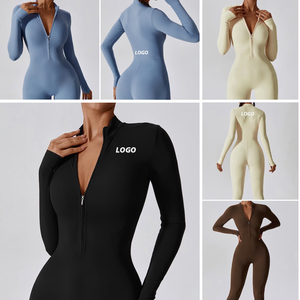 Activewear Tech
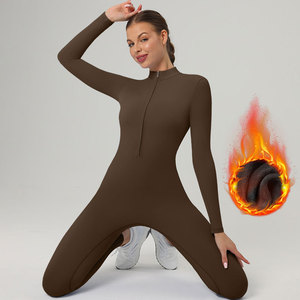 Thermal Fleece Lining
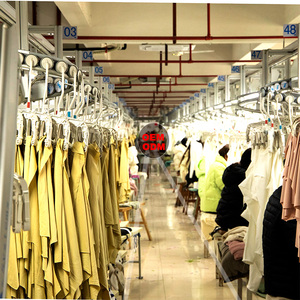 Verified OEM / ODM
In the rapidly modernizing landscape of global apparel procurement, selecting a CE Certified Custom Underwear Manufacturer has evolved from a simple pricing comparison into a comprehensive technical auditing process. Modern intimate apparel—spanning men’s boxers, women’s seamless panties, shapewear bodysuits, thermal base layers, and ergonomic activewear—demands an unprecedented level of material compliance, structural elasticity retention, skin-safe chemical processing, and precision seam construction.
According to recent global textile compliance frameworks, garments worn directly against the skin for extended durations are subjected to rigorous regulatory scrutiny, particularly within the European Economic Area (EEA) under strict CE Marking protocols and EU REACH (Registration, Evaluation, Authorisation and Restriction of Chemicals) Annex XVII regulations. Independent brands, direct-to-consumer (DTC) fashion lines, and established retail chains can no longer rely on unverified suppliers. Modern buyers require production facilities backed by transparent quality engineering, documented lab-dip color fastness, zero-carcinogenic dye guarantees, and strict ISO 9001:2015 quality control management.
E-E-A-T Sourcing Insight: A verified CE Certified factory eliminates legal compliance risks in European and North American markets by ensuring all raw elastane blends, organic combed cottons, bamboo viscose, and synthetic microfiber fabrics pass stringent formaldehyde, heavy metal, phthalate, and pH skin-neutrality testing prior to bulk cutting.
Our manufacturing matrix, operating under the verified production standards established by Tack Apparel & affiliated state-of-the-art facilities, resolves the critical tension between low minimum order quantities (MOQs) and high-volume factory precision. Traditional apparel production forces emerging fashion brands to commit to 1,000+ units per style, tying up essential liquidity in untested inventory. Our modernized, lean manufacturing architecture disrupts this legacy constraint by establishing an accessible 50 pieces per design MOQ while maintaining tier-one industrial quality.
We convert preliminary hand sketches, digital mood boards, or reference garments into production-grade CAD tech packs with complete BOMs (Bill of Materials), graded size charts, seam call-outs, and precise tolerance specs.
Every batch undergoes 1) raw material/trim inspection upon arrival, 2) in-line stitching checks during assembly, 3) 100% spec measurement auditing post-ironing, and 4) final statistical AQL 2.5 quality control before boxing.
Accelerate your product go-to-market cycle with prototype sampling ready in 7 to 12 business days, enabling real-world fit validation, wear-testing, and investor presentation prior to bulk capital commitment.
An intimate apparel product line is defined by its subtle branding touches and tactile luxury. Our integrated private label manufacturing service encompasses every facet of brand presentation: custom woven neck labels, non-irritating heat-transfer tagless care labels, laser-engraved waistband elastics, custom branded polybags, eco-friendly hang tags, and e-commerce-ready exterior packaging. By centralizing custom decoration (including high-density screen printing, DTF, heat sublimation, and precision 3D puff embroidery) under one roof, we guarantee color consistency and zero vendor fragmentation across your entire product line.
As the international textile industry accelerates toward sustainable practices, digitalization, and localized fulfillment, brands sourcing custom underwear and performance apparel must align with three macro development trends reshaping garment procurement.
Traditional cut-and-sew methods are rapidly yielding market share to ultrasonic stitchless bonding and top-gauge seamless circular knitting (utilizing Santoni-type machinery). Bonded seams eliminate skin friction, enhance stretch memory, and offer a zero-bulk fit ideal for modern seamless underwear, shapewear, and activewear bodysuits. Factories equipped with ultrasonic tape-sealing machines deliver superior durability through 50+ industrial wash cycles.
Procurement intent is heavily shifting toward GOTS-certified (Global Organic Textile Standard) cotton, GRS-certified recycled polyester/nylon derived from ocean plastic, and biodegradable TENCEL™ Modal fibers. In intimate apparel, where breathability and moisture management are paramount, eco-conscious fabrics treated with non-toxic, plant-based anti-microbial finishes represent the fastest-growing consumer market segment globally.
To combat inventory overstock and reduce capital expenditure risks, global buyers are abandoning monolithic annual orders in favor of agile, quarter-based capsule drops. Low-MOQ manufacturing hubs capable of scaling seamlessly from 50-piece initial validation runs up to 50,000-unit mass production runs provide DTC brands with the flexibility needed to test niche sizing, seasonal colorways, and specialized functional cuts.
The convergence of athleticwear and intimate apparel has popularized smart thermal regulation. Advanced yarn spinning incorporating phase-change materials (PCM), capillary moisture-wicking channels, and silver-ion antibacterial protection are now essential criteria for high-performance underwear and active bodysuits designed for demanding physical conditions.
To assist procurement managers, technical designers, and apparel brand founders in making informed sourcing decisions, the following data matrix details standard fabric weights, material compositions, elastomeric recovery metrics, and manufacturing timelines across core garment categories.
| Garment Category | Target Fabric Weight (GSM) | Material Composition Options | Compliance & Test Standards | Standard MOQ | Production Lead Time |
|---|---|---|---|---|---|
| Men’s Premium Boxers / Briefs | 160 – 210 GSM | 95% Combed Cotton / 5% Elastane; 93% Micro-Modal / 7% Spandex |
CE Standard, OEKO-TEX 100, REACH Annex XVII |
50 Pcs / Design | 15 – 22 Days |
| Women’s Seamless Panties | 120 – 170 GSM | 85% Recycled Polyamide / 15% Elastane; Bamboo Viscose Blends |
ISO 9001:2015, Anti-Bacterial JIS L 1902 Test Passed |
50 Pcs / Design | 15 – 20 Days |
| Activewear Leggings & Yoga Pants | 220 – 300 GSM | 75% Nylon / 25% Spandex (Double Brushed); 78% Recycled Poly / 22% Lycra |
ASTM D5034 Seam Strength, Squat-Proof Opacity Audited |
50 Pcs / Design | 18 – 25 Days |
| Performance Bodysuits & Jumpsuits | 240 – 320 GSM | Four-Way Stretch Poly-Spandex; Thermal Interlock Fleeced Knits |
Color Fastness Grade 4+, Shrinkage < 3% Post Wash |
50 Pcs / Design | 20 – 28 Days |
| Heavyweight Streetwear T-Shirts | 220 – 280 GSM | 100% Organic Ring-Spun Cotton; Bio-Washed Heavy Jersey |
GOTS Organic Certified, Formaldehyde-Free Dyes |
50 Pcs / Design | 15 – 20 Days |
| Cut & Sew Hoodies & Tracksuits | 320 – 500 GSM | 100% Cotton French Terry; Heavy Brushed Fleece 80/20 |
Rubbing Fastness ISO 105-X12, Anti-Pilling Grade 4 |
50 Pcs / Design | 20 – 30 Days |
Below are authoritative responses to critical questions encountered by supply chain executives, apparel developers, and retail buyers during factory evaluation and order initiation.
To achieve full compliance, a manufacturer must ensure that all raw materials, dyes, elastic bands, and finishing agents comply with European Union directives regarding skin-contact consumer goods. This involves rigorous testing for azo dyes, heavy metals, nickel release (on snaps/zips), phthalates, and formaldehyde under REACH regulations. Furthermore, production processes are audited under ISO 9001 and BSCI ethical labor guidelines to guarantee safety, quality, and human rights compliance.
Our minimum order quantity of 50 pieces per design allows emerging fashion brands to test market demand without heavy capital risk. The 50-piece minimum can typically be split across up to 5 standard sizes (e.g., XS, S, M, L, XL) and up to 2 distinct fabric colorways (e.g., 25 black units / 25 navy units), provided the base fabric composition and cut pattern remain identical.
Yes. Our in-house technical design division specializes in transforming preliminary hand sketches, digital illustrations, CAD mockups, or physical reference garments into factory-ready tech packs. We construct detailed measurement grading tables, specify recommended fabric GSMs, detail seam construction type (e.g., 4-needle 6-thread flatlock), and define custom branding specs prior to sample cutting.
Once your tech pack and fabric lab-dips are approved, proto-type sample creation takes approximately 7 to 12 business days. Following final pre-production sample (PPS) sign-off, bulk factory production runs between 15 and 30 business days depending on order volume, fabric customization, and decoration complexity. Express air freight and DDP (Delivered Duty Paid) door-to-door delivery are available for tight launch deadlines.
Quality control is built directly into our assembly line workflow across four distinct inspection gates: 1) Initial raw fabric roll testing (checking GSM, color uniformity, and shrinkage), 2) In-line stitching inspections at key stress points, 3) 100% spec sheet measurement audits following steam pressing, and 4) Final AQL 2.5 statistical sampling inspection prior to polybagging and carton sealing.
We offer comprehensive private label solutions designed to make garments 100% e-commerce and retail-ready upon arrival. Options include heat-transfer tagless neck logos, woven satin tags, custom jacquard elastic waistbands, branded hang tags with string locks, individual eco-polybags with barcode stickers, and custom printed shipper boxes.
Achieving flawless garment construction requires strict adherence to a standardized manufacturing protocol. Our factory operations follow a six-stage methodology engineered to mitigate production risk, preserve fabric elasticity, and guarantee delivery timeline precision:
Digitization of pattern blocks, precise grading across size spectrums, and creation of automated CAD markers to optimize fabric consumption efficiency and reduce waste.
Dyeing fabric swatches to exact Pantone matching standards, followed by lab testing for wash-shrinkage rate, color fastness against sweat/light, and tensile stretch recovery.
Creation of Pre-Production Samples (PPS) using actual bulk fabric and trims. Physical fitting sessions evaluate ergonomic stretch, seam strength, and aesthetic appeal.
Computerized laser blade fabric cutting followed by specialized assembly using flatlock, coverstitch, overlock, or ultrasonic seam bonding machinery.
Application of high-density prints, silicone grip tapes, tagless transfers, or custom jacquard elastics, completed with professional steam pressing and shaping.
Final statistical quality audit, barcode labeling, polybag packing, and direct dispatch via air express or ocean freight with full customs clearance support.