 Talk to production646-681-4212 Talk to production646-681-4212
Explore our export-ready technical apparel solutions engineered for rigorous industrial compliance, high-visibility safety, and custom brand identity.
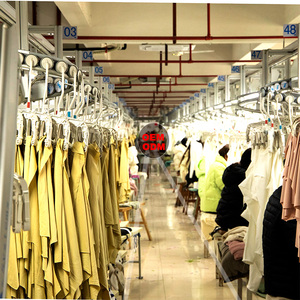
In modern industrial procurement, navigating the global compliance ecosystem requires rigorous technical validation. As a premier CE Certified Custom Workwear Exporter & Exporter, Tack Apparel establishes a baseline of regulatory rigor aligned with the Personal Protective Equipment (PPE) Regulation (EU) 2016/425 and North American OSHA mandates. High-performance workwear is no longer merely transactional corporate attire; it is an active hazard-mitigation layer engineered to safeguard workforce ergonomics, thermal regulation, and structural integrity across demanding workplace environments.
European Conformity (CE Marking) serves as an imperative declaration that exported garments adhere to stringent health, safety, and environmental protection benchmarks. Sourcing directors, safety procurement managers, and corporate brand wholesalers must evaluate workwear exporters based on certified testing protocols across five foundational Harmonized European Standards:
Specifies requirements for high-visibility workwear capable of visually signaling the user's presence. Evaluates retroreflective tape luminance, background fluorescent material chromaticity, and minimum surface area classes (Class 1, Class 2, Class 3).
Mandates protective performance against radiant, convective, and contact heat, as well as molten metal splash. Covers limited flame spread (A1/A2), convective heat (Code B), and radiant heat exposure (Code C).
Measures garment resistance to water penetration (hydrostatic pressure head test ISO 811) and water vapor resistance (breathability RET index ISO 11092) for exterior foul-weather gear.
To eliminate compliance risks for importers in North America, Europe, Australia, and the Middle East, our production facilities integrate certified lab testing during raw material sourcing. Every mill lot of canvas, high-tenacity polyamide, or stretch twill undergoes lab dip validation, tensile tear strength testing (ISO 13937), and color-fastness audits under ISO 105 protocols prior to marker making and cut-and-sew assembly.
For technical buyers comparing global workwear manufacturers, understanding fabric weight (GSM), fiber composition, tensile durability, and compliance classes is crucial to optimizing landed unit costs against field longevity. Below is our standard manufacturing benchmark matrix:
| Workwear Category | Primary Fabric Blend | GSM Range | CE & International Standard | Key Durability Features |
|---|---|---|---|---|
| High-Vis Executive Jackets | 100% Recycled Polyester Oxford 300D | 180 – 240 GSM | EN ISO 20471 Class 3, EN 343 4:4 | PFAS-free DWR coating, 3M Scotchlite tape, sealed seams |
| Heavyweight Industrial Crew Shirts | 100% Combed Cotton / CVC Blend | 220 – 260 GSM | OEKO-TEX Standard 100, EN 13758 UPF 50+ | Double-needle collar, reactive dye, anti-pilling, pre-shrunk |
| Flame-Retardant Coveralls | 99% Cotton, 1% Antistatic Fiber (Proban) | 300 – 380 GSM | EN ISO 11612, EN 1149-5 (Antistatic) | Triple-stitched main seams, brass hardware, radio loops |
| Tactical & Utility Work Pants | 65% Poly / 35% Cotton Ripstop Twill | 240 – 280 GSM | ISO 13934-1 Tensile Strength Certified | Cordura-reinforced knee pockets, gusseted crotch, 10 pockets |
| Thermal Fleece Inner Layers | 100% Micro-Polar Polyester Fleece | 280 – 400 GSM | EN 342 (Cold Insulation protection) | Anti-static finish, YKK zip hardware, windproof lining |
This technical transparency ensures that enterprise buyers can match their internal spec sheets directly to verified material performance indicators without risking field failures or import delays at customs checkpoints.
The global workwear market is undergoing a structural transition driven by corporate ESG (Environmental, Social, and Governance) targets, regulatory decarbonization mandates, and digitalized supply chain tracing. B2B procurement managers are shifting away from disposable, low-cost safety apparel toward sustainable, technology-integrated work garments designed for extended lifecycles. Key developments shaping future procurement include:
With the European Union’s Strategy for Sustainable and Circular Textiles coming into full enforcement, procurement policies increasingly favor garments containing post-consumer mechanically recycled polyester (rPET) and chemically recycled polyamides. Future CE-marked workwear must maintain high tensile strength while achieving low-carbon footprints. Exporters capable of providing GRS (Global Recycled Standard) certification documentation alongside CE test reports hold a decisive competitive advantage.
Industrial laundry facilities and enterprise logistics fleets are adopting passive UHF RFID transponders embedded within garment hems. These smart tags allow enterprises to track wash cycles, monitor flame-retardant coating degradation, automate inventory check-outs, and verify full supply chain traceability from raw fiber origin to garment disposal.
Traditional manufacturing models required massive order volumes (1,000+ pieces per style), forcing distributors to carry heavy inventory carrying costs. Modern enterprise procurement favors dynamic, low-MOQ sourcing models—such as our standard 50-piece minimum per design—allowing buyers to launch niche workforce sizing, validate custom corporate colorways, and scale orders dynamically based on real-time workforce growth.
Advancements in textile engineering and digital apparel manufacturing have unlocked unprecedented performance metrics for custom workwear exporters. Key technological innovations engineered directly into our cut-and-sew lines include:
Replacing toxic fluorinated chemicals (PFAS/PFOA) with eco-friendly bio-based fluorine-free water repellent coatings that maintain hydro resistance above 10,000 mm ISO 811 after 30 industrial wash cycles.
Utilizing 3D CAD digital pattern engineering to incorporate articulated elbow seams, gusseted crotches, and dynamic stretch panels that eliminate fabric binding during overhead reaching and squatting.
Integrating graphene-infused matrix linings into cold-weather work jackets to distribute body heat evenly, dissipate static buildup, and reduce overall garment weight by up to 30% compared to traditional batting.
As an established custom clothing manufacturer and global exporter, Tack Apparel addresses the systemic operational friction points that B2B importers experience with overseas factories. Our end-to-end infrastructure unites design development, raw material lab testing, pattern grading, cut-and-sew assembly, custom decoration, private label branding, and international DDP (Delivered Duty Paid) shipping under a single accountable engineering team.
To ensure 100% spec accuracy across all production runs, every batch follows a strict four-inspection gate standard operating procedure:
In-house pattern makers convert client sketches or tech packs into accurate 2D/3D CAD markers, measurement charts, and stitch spec sheets before fabric cutting begins.
Fabrics and trims are audited upon arrival for GSM density, color accuracy against Pantone standards, tensile tear strength, and chemical safety certification.
A physical fit proto sample is sewn in 7–12 days and dispatched for client sign-off. Production line tooling and decoration screens are locked only after approval.
Quality inspectors execute live audits on seam strength, needle gauge tension, seam sealing, and embroidery stitch density directly on active sewing lines.
Finished garments undergo random statistical sampling according to ISO 2859-1 (AQL 2.5) standards to verify sizing tolerance, labeling, trim placement, and clean finishing.
Items are packed with custom woven labels, care tags, barcoded polybags, and heavy-duty corrugated cartons prior to air express or sea container freight dispatch.
Whether you require a initial 50-piece capsule order for market validation or a 20,000-unit repeat production run, our single-point merchandising workflow ensures complete specification continuity without color drift or sizing variance.
Clear, transparent answers to the critical technical and logistical questions asked by safety directors, wholesale buyers, and apparel brand founders prior to placing custom workwear export orders.
Ready to engineer custom high-performance workwear or launch your private label apparel collection? Speak directly with our production specialists today for fast quotes, tech pack audits, and sample arrangements.
Contact Us