 Talk to production646-681-4212 Talk to production646-681-4212
Explore our export-ready OEM/ODM manufacturing capability across customized knitwear, activewear, fleece, and technical performance garments. Engineered for private label scalability.
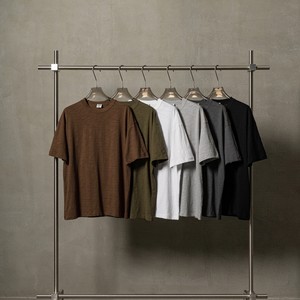
Combed ring-spun cotton, pre-shrunk finish, 180-240 GSM options with double-needle hems.
Bespoke paneling, heavy French terry fleece 320-450 GSM, customized hardware and ribbed trims.
High-density 3D puff embroidery, Tajima machine precision, color-fast thread matrix.
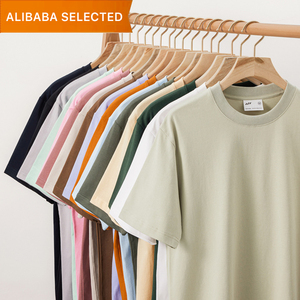
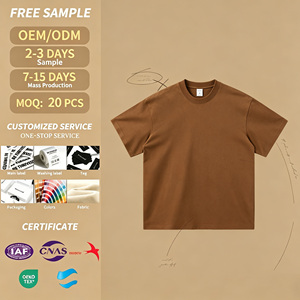
250 GSM heavy jersey, oversized boxy silhouette, reinforced collar rib, reactive garment dyeing.
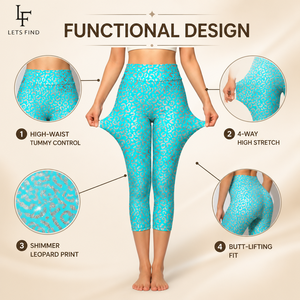
Double-brushed Nylon/Spandex, squat-proof opacity, 4-way stretch, flatlock anti-chafing seams.
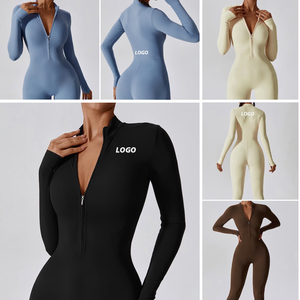
Ergonomic compression contouring, invisible auto-lock zip, moisture-wicking quick-dry treatment.
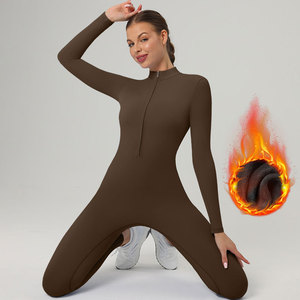
Thermal-brushed lining, butt-lifting structural seamwork, cold-weather stretch insulation.
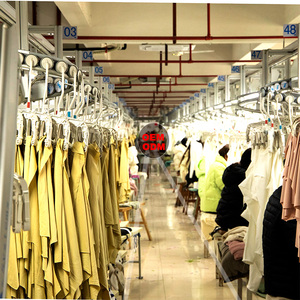
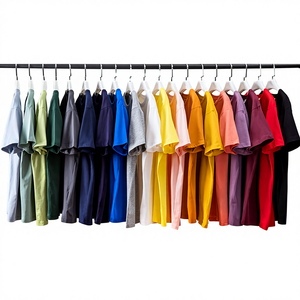
Full OEM/ODM customization, private label neck branding, hangtag integration, retail-ready polybags.
From initial digital tech pack translation to audited mass cut-and-sew manufacturing, our integrated production lines bridge the gap between creative design concepts and high-velocity retail delivery.
Don't have a technical file? Our in-house apparel engineers convert flat sketches, physical reference garments, or mood boards into production-ready tech packs complete with precise BOM (Bill of Materials), stitch density call-outs, trim specifications, and size grading formulas.
Scale without over-capitalizing. Our flexible low minimum order quantity of 50 pieces per design allows boutique retailers, DTC startups, and corporate clients to validate market demand, test niche fits, and deploy rapid seasonal drops without high inventory liability.
Every garment undergoes strict quality control protocols: 1) Raw mill fabric inspection & shrinkage testing, 2) In-line stitching checks, 3) Dimensional measurement audit against tech pack tolerance, and 4) Final pre-shipment AQL 2.5 standard packing inspections.
Understanding structural shifts in fabric engineering, digital sampling workflows, and consumer expectation curves in modern garment sourcing.
The global streetwear and premium leisure markets have undergone a fundamental shift toward higher fabric weights and specialized surface textures. Buyers are moving away from standard lightweight 140 GSM promotional tees in favor of heavyweight 240 to 300 GSM combed cottons and 400+ GSM French terry fleeces. In activewear, moisture management is no longer a superficial coating; high-performance fabrics now utilize multi-channel polyester/nylon cross-sections paired with high-gauge elastane to achieve permanent sweat-wicking, squat-proof opacity, and anti-microbial properties.
As an experienced OEM/ODM apparel exporter, our mills utilize specialized bio-polishing, enzyme washes, and silicone finish baths that elevate the tactile hand-feel of organic cottons, prevent pilling after repeated laundering cycles, and stabilize dimensional shrinkage below 3% across vertical and horizontal grain lines.
By leveraging 3D digital pattern software, we simulate fabric drape, stretch deformation, and stress-point friction on virtual 3D avatars before cutting physical cloth. This reduces sample revision cycles by up to 60%, drastically minimizing fabric waste and speeding up prototype approval timelines.
Global buyer demand for sustainability has pushed ODM factories to adopt GOTS-certified organic cottons, Recycled Polyester (rPET) derived from post-consumer ocean plastics, and OEKO-TEX Standard 100 certified low-impact reactive dyes that eliminate toxic heavy metals and azo compounds.
Modern streetwear design merges traditional cut-and-sew construction with hybrid decoration methods: combining Direct-to-Film (DTF) high-definition photographic prints with chenille embroidery patches, flocking, screen-printed high-density rubber, and puff ink finishes.
Standard commercial cotton fabrics undergo 5-8% post-wash shrinkage if untreated. Our contract manufacturing process incorporates a mandatory tubular stenter compaction and pre-shrunk steam bath treatment during fabric finishing. This guarantees that your customized 250+ GSM T-shirts and hoodies maintain their exact graded spec measurements through institutional and domestic laundering cycles.
Navigating geopolitical shifts, supply chain transparency requirements, and agile inventory models in overseas garment procurement.
The era of locking capital into 10,000-unit single-style production runs 9 months ahead of season is being rapidly replaced by micro-capsule replenishment models. DTC brands and boutique exporters utilize lower initial MOQs (50–200 units) to test product-market fit across multiple colorways and silhouettes. Once sell-through rates are established via real-time e-commerce analytics, rapid-turnaround OEM suppliers scale re-orders within 15–20 days using pre-reserved grey fabric stock.
Regulatory frameworks in North America and the European Union are mandating full supply chain transparency. Future apparel sourcing requires detailed documentation tracing raw fiber origin (e.g., U.S. Cotton, Egyptian Long-Staple, recycled synthetic yarn), chemical management compliance (REACH), and ethical labor audit certifications (BSCI, WRAP, SEDEX). Verified OEM vendors provide digitized chain-of-custody certificates alongside bulk shipments.
To hedge against maritime freight delays and localized trade tariffs, enterprise procurement directors are adopting a multi-hub sourcing approach. High-complexity, high-tech activewear and specialized outerwear are allocated to specialized manufacturing centers with integrated vertical knitting mills, while fast-turn replenishment lines utilize regional logistics pathways with DDP (Delivered Duty Paid) air freight support.
Advanced OEM exporters integrate automated pattern-nesting algorithms that optimize fabric marker efficiency to over 88-92%. By reducing cutting table wastage, factories minimize raw material consumption per garment—passing direct unit cost savings onto buyers while reducing post-industrial textile waste.
Comprehensive technical specification guidelines for procurement officers and apparel production managers.
| Apparel Category | MOQ (Per Design) | Recommended Fabric Specs | Customization Options | Lead Time (Proto / Bulk) |
|---|---|---|---|---|
| Heavyweight T-Shirts | 50 Pcs | 180 - 280 GSM 100% Combed Cotton / Single Jersey | Screen Print, DTF, Puff Print, Vintage Wash, Custom Tags | 7 Days / 15-20 Days |
| Streetwear Hoodies | 50 Pcs | 320 - 500 GSM French Terry or Brushed Fleece | Bespoke Cut & Sew Paneling, Chenille Embroidery, Custom Hardware | 8 Days / 20-25 Days |
| Yoga & Activewear | 50 Pcs | 220 - 300 GSM Nylon/Spandex or Recycled Polyester | 4-Way Stretch, Flatlock Stitching, Heat-Transfer Reflective Logos | 10 Days / 20-30 Days |
| Denim Apparel | 100 Pcs | 11 - 14 oz Cotton Rigid or Stretch Denim | Enzyme Wash, Laser Distressing, Custom Leather Back Patches, Rivets | 12 Days / 25-35 Days |
| Corporate & Team Uniforms | 100 Pcs | Poly-Cotton Twill, PV Suiting, Oxford Weave | Precision Embroidered Crests, Stain-Resistant Coating, Name Tags | 7 Days / 20-30 Days |
| Leather Goods & Outerwear | 30 Pcs | Real Cow/Sheep Leather, Eco-PU Vegan Leather | Custom Lining Printing, Embossed Logos, YKK Metal Zippers | 12 Days / 30-40 Days |
Submit CADs or samples. Receive itemized cost sheets detailing fabric, trims, labor, and logistics options.
Pantone color matching (Lab Dips) and pre-production sample creation within 7-12 business days.
Precision fabric cutting, automated stitching lines, mid-production inline checks, and final AQL 2.5 audit.
Expert solutions to common procurement, technical customization, and export compliance queries.
Connect directly with our senior apparel engineering team. Share your tech packs, design sketches, or sourcing inquiries to receive custom price quotes within 24 hours.